


Sumber Waja offers a complete range of SIHI liquid & vacuum pumps as well as other products for many applications in the chemical, pharmaceutical, power, water and waste water, food and beverage, rubber and plastic, steel, pulp and paper and machinery manufacturer industries.
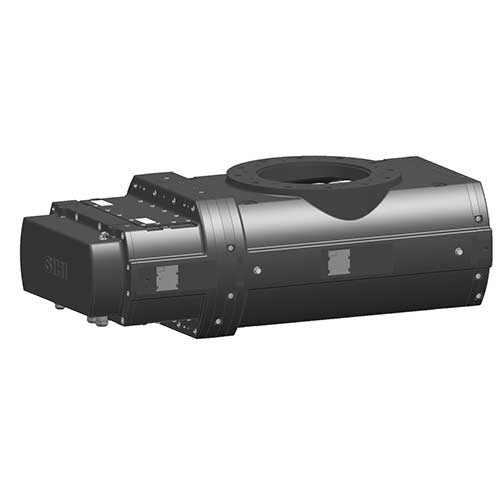 SIHI Boost – PB-Systems are designed for chemical and pharmaceutical markets where an explosion proof design is required. SIHI Boost is a dry screw vacuum booster, which provides deep vacuum levels with less power and a smaller footprint. The rotors run five times faster than typical machinery, it is quieter, safer and cleaner. Mechatronically synchronized, contact-free moving parts reduce the need for oil-centric lubrication.
 SIHI Boost – CB-Systems are designed for a broad range of industrial applications where an encapsulated, integrated pumps system design is required. SIHI Boost is a dry screw vacuum booster, which provides dramatically quicker evacuation at deep vacuum levels with less power and a smaller footprint. By harvesting the kinetic energy of heavier rotors that run five times faster than typical machinery, it is quieter, safer and cleaner. Mass inertia is stored during idle periods and can be released immediately.

SIHI Boost – GB-Systems are designed for a broad range of industrial applications. The vacuum systems combine independent components mechanically to offer optimized modular solutions matching actual process requirements. SIHI Boost is a dry screw vacuum booster, which provides dramatically quicker evacuation at deep vacuum levels with less power and a smaller footprint.
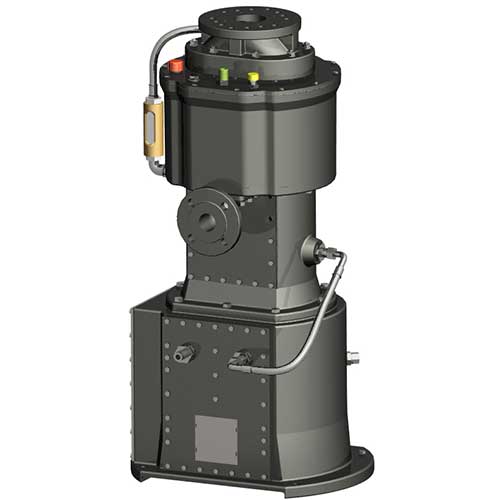
SIHI Dry – PD-Systems are designed for chemical and pharmaceutical markets where an explosion proof design is required.The SIHI Dry is a vertically oriented and self draining vacuum pump with no mechanical shaft seals. It is an ideal choice for chemically related processes where there is a high possibility of liquids or solids carry-over. This award winning solution can accommodate corrosive gases and vapors, and has superior resistance to heat-accelerated deposition.
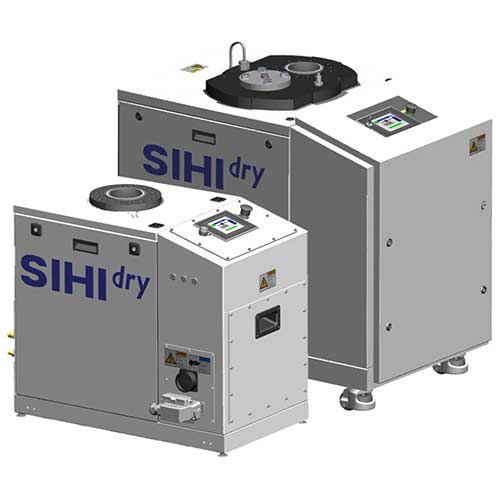
SIHI Dry – CD-Systems are designed for a broad range of industrial applications where an encapsulated, integrated pumps system design is required. Vertically oriented, and self-draining, makes the SIHI Dry ideal for industrial process where there is a high possibility of solids being carried over into the pump. Stand alone capacity ranges from 100 up to 1500 m³/h (60 up to 900 cfm), and can be increased dramatically by combining with SIHI Boost.

SIHI Dry – GD-Systems are designed for a broad range of industrial applications. The SIHI Dry is a vertically oriented and self draining vacuum pump with no mechanical shaft seals. It is an ideal choice for chemically related processes where there is a high possibility of liquids or solids carry-over. This award winning solution can accommodate corrosive gases and vapors, and has superior resistance to heat-accelerated deposition.
SONY DSC
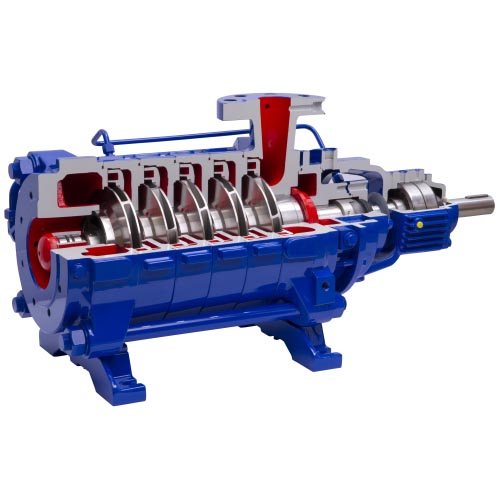
The MSC is a highly efficient ring section pump with patented balancing system, extremely low NPSH, with a wide range of hydraulics and materials.
 The MSH is a highly efficient ring section pump with combination balance drum and flange, extremely low NPSH, with a wide range of hydraulics and materials.
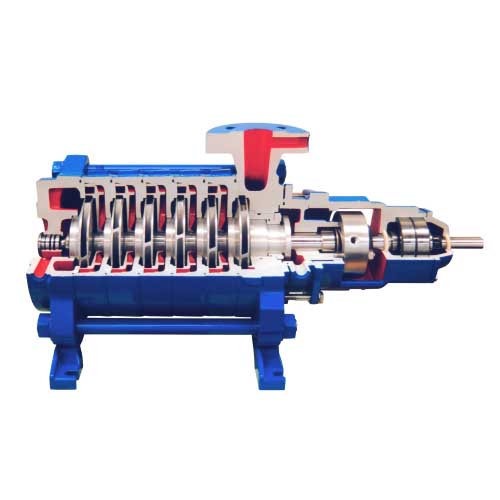
The MSM / MSL line is a highly efficient ring section pump with patented balancing system, extremely low NPSH, with a wide range of hydraulics and materials.
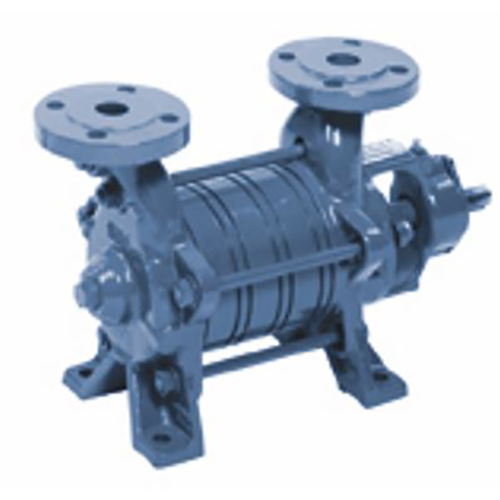
The ADH pumps are self-priming side channel pumps capable of handling gas and medium while operating at a low noise level. These pumps have a segmental construction with open vane wheel impellers. The ADH series run at high speed and have been designed with special regard to noiseless running. The program comprises of 6 sizes.

Pumps of the series AEH-X/AEH according to EN 734 have a segmental type construction with open vane wheel impellers. This pump is available in a normal industrial design with one liquid surrounded slide bearing and one ball bearing, or in a heavy-duty construction with a double ball bearing design.
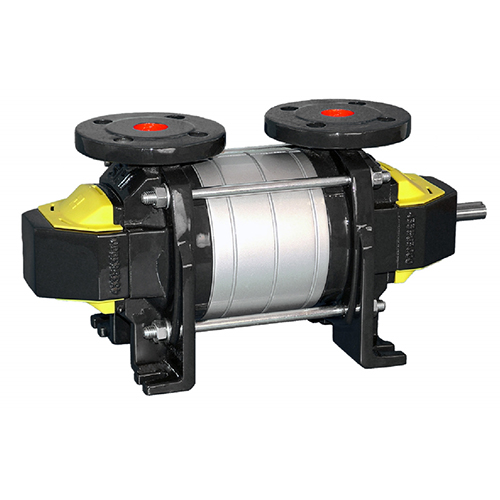
Pumps of the series AKH-X/AKH have a segmental type construction with open vane wheel impellers. The pump construction is either with one liquid surrounded slide bearing and one ball bearing or in a more industrial construction by using a double ball bearing design.

Pumps of the AOH Industrial Process and Chemical Pumps series have a segmental type construction with open vane wheel impellers.
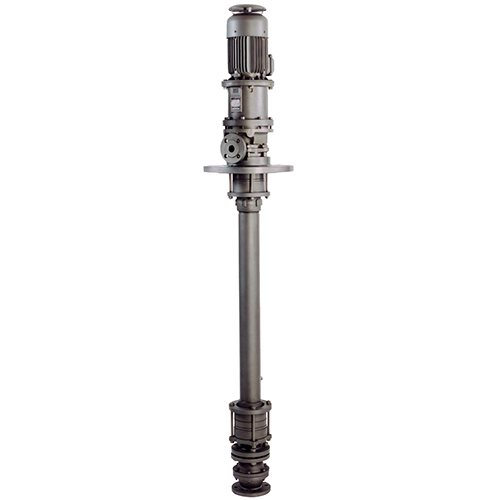
The CEB side channel units are a low noise design of combination pumps. They are ideal for pumping liquids that are stored at their boiling point, have a degree of entrained gas, or very low NPSH conditions. The vertical tank pump has been designed in order to enable retro-fitting into most common tanks. Moreover, the dimensions are such that the unit can be used to replace submersible designs of pumps. Although the pump can be supplied in other lengths, the standard size is between 1.3 and 3.0 m.
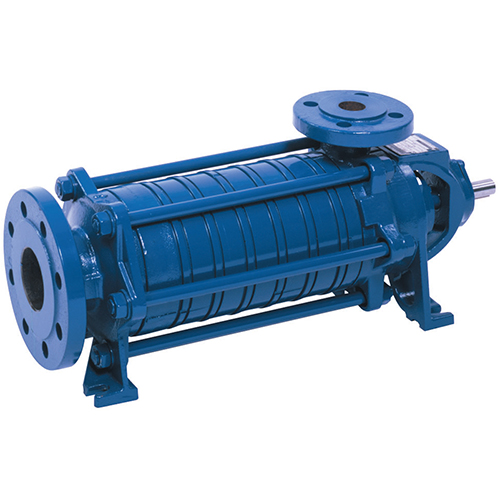
Pumps of the series CEH-X/CEH have a segmental type construction with open vane wheel impellers. The construction of the CEH pump is a so-called centrifugal combined system. This combination pump is suited with a centrifugal stage serial connection before the side channel stages in order to obtain a more favorable NPSH.

Superior hot water circulation, up to 230°C (446°F) with a standard un-cooled mechanical seal, gives the unique ability to minimise life-cycle cost. Internal separation and removal of undesirable vapour (steam) enhances mechanical seal face lubrication and improves reliability. High-level hydraulic efficiency ensures that running cost are predictably low.
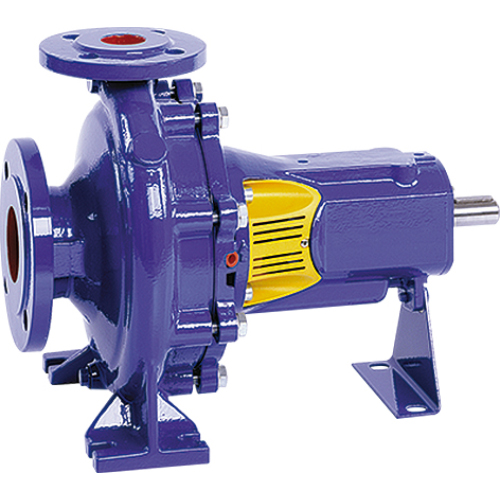
ZLN, ZLK, ZLI industrial process pumps are suitable for temperatures up to 170°C (338°F). This diverse range of general purpose pumps offers the user a low life-cycle cost solution. Capital cost, power consumption, maintenance, reliability and waste, have all been considered during the extensive development phase.
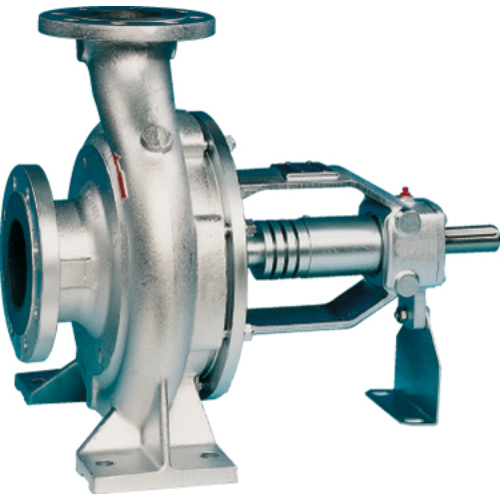
Operational safety, environmental concern and long-term reliabilty, are the three aspects which make this pump an ideal choice for thermal oils up to 350°C (662°F). High-end hydraulic efficiency is complimented by almost maintenance-free operation, in which to give a low Life-Cycle cost solution. Shaft sealing can be either a combiniation of mechanical and secondary lip seals.
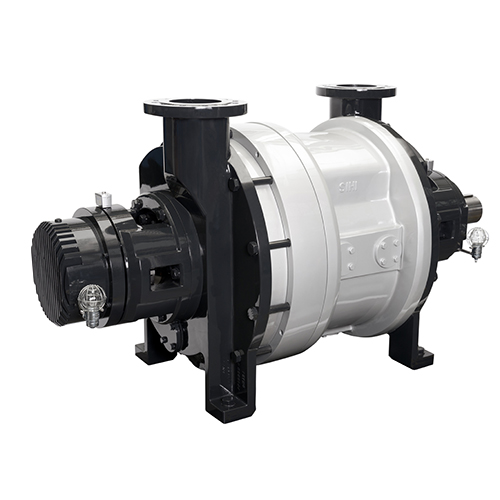
Liquid ring compressors of the series KPH are one to three-stage displacement compressors of simple and robust construction.
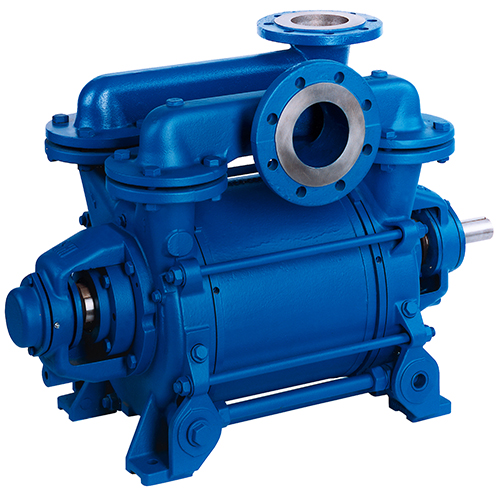
Liquid ring vacuum pumps of the series LEH are single-stage displacement pumps and have a simple but robust construction.

Liquid ring vacuum pumps of the series LPHX/LPH are two-stage displacement pumps with a simple but robust construction.
 The standard chemical process pumps of the CBE/CBM range are horizontal, single-stage volute casing pumps with dimensions to ISO 2858 and meet the technical requirements of ISO 5199 and ISO 15783.
 The CBT is a horizontal, single-stage volute casing pump with ISO 2858/5199 design features and nominal rating. Engineered for applications in chemical,
petrochemical and pharmaceuticals processing with flows beyond the range defined by ISO 2858.